#4 – 20133 102nd Avenue, Langley, B.C. V1M 4B4 Canada
#4 – 20133 102nd Avenue, Langley, B.C. V1M 4B4 Canada
Choosing among China’s best rapid prototyping companies requires more than comparing prices on a supplier website. Global buyers need dependable communication, controlled production, and evidence of consistent quality. A polished sample may look impressive, yet the real test begins when drawings change, tolerances tighten, or delivery schedules become difficult.
This guide examines how leading Chinese suppliers support international product teams. It considers CNC machining, 3D printing, vacuum casting, sheet metal fabrication, and finishing services. Practical details matter. Can a supplier produce a clean aluminum bracket with accurate holes? Can it deliver an SLA resin enclosure without visible layer defects? Are inspection reports, material certificates, and revision records available when requested? These questions reveal more than promotional claims. They also show whether a company has experience serving demanding global buyers.
No supplier is perfect.
Our evaluation focuses on technical capability, production capacity, quality systems, communication, pricing transparency, and export experience. Certifications such as ISO 9001 may support credibility, but buyers should verify their scope and validity independently. Lead times can also change because of material availability, engineering revisions, or shipping conditions. That reality deserves attention. A low quotation may hide weaker inspection procedures or expensive rework later. Conversely, the highest price does not automatically guarantee the best result.
The companies discussed here are presented as practical options for different project needs, from early prototypes to small-batch validation. Buyers should still request samples, confirm tolerances, review non-disclosure terms, and approve a clear production specification before placing an order. Reliable partnerships develop through documented processes, honest feedback, and measurable results—not promises alone.
China’s rapid prototyping market is expanding within a $20.0 billion global additive manufacturing industry. Wohlers Associates reported that the global AM sector reached approximately $20.0 billion in 2023. This figure includes printers, materials, software, and services, not prototype production alone. That distinction matters for buyers comparing suppliers.
China offers dense manufacturing networks, broad material access, and competitive production costs. Buyers can request CNC machining, SLA, SLS, metal printing, and vacuum casting from one sourcing region. However, speed should not replace verification. A low quotation may hide limited inspection, weak surface finishing, or unclear material traceability.
Technical drawings should define tolerances, surface requirements, testing methods, and acceptance samples. ISO 9001 certification can support process control, but it cannot guarantee every part’s quality.
Tips: Ask for a documented quality plan, dimensional inspection records, and material certificates. Confirm lead times with production and shipping buffers. For safety-sensitive components, request independent testing when appropriate. A small pilot order often reveals more than a polished presentation.
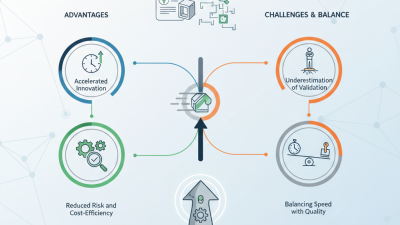
Market forecasts remain optimistic, yet rapid prototyping is not automatically cost-effective. Complex geometries may reduce tooling needs, while simple parts can remain cheaper through conventional methods. Buyers should compare total cost, including revisions, finishing, freight, and quality failures. That comparison is sometimes overlooked.
Global buyers need rapid prototypes that do more than look accurate on a screen. In practice, process selection shapes surface quality, strength, lead time, and cost. CNC machining suits functional parts requiring tight fits and durable surfaces. SLA produces fine details and smooth visual models, although brittle sections need careful handling. SLS supports complex polymer forms without traditional support structures. SLM builds dense metal components layer by layer, but thermal stress and post-processing demand experienced control. These differences matter when a prototype moves toward testing.
A ±0.05 mm accuracy target sounds clear, but it is not universal. It depends on material, feature size, tool condition, machine calibration, orientation, and measurement method. Experienced teams confirm critical dimensions before production, then use calibrated gauges or coordinate measurement equipment for verification. They also review drawings, tolerances, wall thickness, and assembly interfaces with the buyer. Small details count. A hole may meet its stated size while a warped mating face still causes failure. Practical engineering judgment often matters more than an impressive specification.
Reliable suppliers document inspection results, communicate deviations, and protect revision control across international orders. Clear files and realistic tolerances reduce avoidable rework. Still, no workshop eliminates every risk. Surface finish may vary, and first-article results can reveal assumptions missed during design. A useful workflow leaves room for correction. Buyers should request material certificates, inspection reports, sample photos, and a defined approval point before volume production. Fast is helpful. Repeatable is better.
| Core Technology | Process Category | Typical Materials | Typical Dimensional Accuracy* | Surface Finish | Typical Lead Time | Best-Suited Applications | Global Buyer Considerations |
|---|---|---|---|---|---|---|---|
| CNC Machining | Subtractive manufacturing | Aluminum, steel, stainless steel, brass, copper, titanium, engineering plastics | ±0.05 mm is commonly achievable tighter tolerances may require controlled processes and inspection |
Approximately Ra 0.8–3.2 µm in common finishing conditions; polishing and bead blasting are available | About 3–15 working days, depending on geometry, material, quantity, and finishing | Functional prototypes, precision housings, jigs, fixtures, end-use metal and plastic parts | Confirm datum references, GD&T requirements, material certificates, inspection reports, and export packaging |
| SLA | Vat photopolymerization | Standard resin, tough resin, clear resin, high-temperature resin, castable resin | Typically about ±0.10–0.20 mm for the first 100 mm, subject to geometry and orientation | Smooth surface with visible layer lines after printing; sanding, painting, and clear polishing are possible | About 2–7 working days | Visual prototypes, fine-detail models, master patterns, display parts, and fit-check components | Ask about resin data sheets, UV stability, brittleness, heat resistance, support marks, and post-curing controls |
| SLS | Powder-bed fusion | PA12 nylon, PA11 nylon, glass-filled nylon, TPU in selected systems | Typically about ±0.20–0.30 mm for the first 100 mm, influenced by shrinkage and part orientation | Uniform, slightly grainy powder-textured surface; dyeing, vapor smoothing, and coating may be available | About 3–10 working days | Durable functional prototypes, snap-fits, lightweight structures, ducting, and low-volume plastic parts | Verify wall-thickness rules, powder refresh policy, dimensional compensation, nesting strategy, and color consistency |
| SLM | Metal powder-bed fusion | Aluminum alloys, stainless steel, tool steel, titanium alloys, nickel-based alloys | Typically about ±0.10–0.20 mm for the first 100 mm; critical surfaces generally require machining | As-built surfaces are rougher than machined surfaces; machining, shot blasting, heat treatment, and polishing may be specified | About 7–25 working days, including heat treatment and post-machining where required | Complex metal parts, topology-optimized components, internal channels, aerospace and medical development parts | Request powder batch traceability, density data, heat-treatment records, CT or dimensional inspection when applicable |
| CNC + Secondary Finishing | Machining with post-processing | Metals and engineering plastics compatible with anodizing, plating, painting, passivation, or polishing | ±0.05 mm target available for defined critical features final capability depends on material, size, machine, and inspection method |
Anodized, plated, powder-coated, painted, brushed, polished, passivated, or chemically treated | About 7–20 working days | Production-intent prototypes, cosmetic enclosures, assemblies, and customer-validation samples | Define color standards, coating thickness, masking areas, cosmetic zones, sampling plans, and acceptance criteria |
| Inspection & Quality Control | Measurement and verification service | Applicable to CNC, SLA, SLS, SLM, and finished assemblies | Capability should be stated against drawing tolerances rather than as a universal value | Visual inspection plus dimensional, surface, material, and functional checks as specified | Usually included in the manufacturing lead time; advanced reports may add 1–5 working days | First-article inspection, pre-shipment approval, tolerance validation, and supplier qualification | Specify calibrated equipment, sampling level, inspection datum, report format, photos, and nonconformance procedure |
Global buyers often rank rapid prototyping suppliers by speed alone. That approach can mislead purchasing teams. A practical ranking should compare lead time, minimum order quantity, production capacity, and total cost.
For CNC prototypes, a common lead-time benchmark is three to seven working days. Vacuum casting may require seven to twelve days. Complex molded parts often need three to six weeks. These figures are planning references, not guarantees.
MOQ strongly affects the ranking. Prototype-focused workshops may accept one to ten pieces, while larger factories often prefer fifty or more. Capacity also matters during product launches. A supplier producing 500 parts monthly may suit testing, but not a 20,000-piece release. Ask for machine lists, monthly output, shift patterns, and recent capacity records.
Cost comparisons should include tooling, finishing, inspection, packaging, and freight. A lower unit price can hide expensive setup charges.
Reliable evaluation requires evidence. Request a sample report, material certificate, dimensional inspection data, and clear revision control. Compare quotations using the same drawings and tolerances.
Communication quality is another useful signal. Slow replies can become costly after production starts. I have found that quoted lead times sometimes exclude approval delays. That deserves scrutiny.
A perfect ranking is impossible because project complexity changes every result. Suppliers should be scored against the buyer’s actual part, volume, tolerance, and delivery risk.
China Best Rapid Prototyping Companies for Global Buyers
Quality verification should begin with evidence, not attractive samples. ISO 9001 shows that a supplier controls documented processes, corrective actions, and customer feedback. Buyers should check the certificate’s scope, site address, and expiration date. A valid certificate may not cover every workshop or production line. That detail is easy to miss.
For automotive prototypes and low-volume parts, IATF 16949 offers stronger process discipline. Request control plans, inspection records, material traceability, and measurement-system studies. A capable supplier should explain how design changes reach operators without confusion. Ask for first article inspection reports. Review them against drawings, tolerances, and revision levels.
Cpk ≥1.33 is a useful process-capability benchmark when the process is stable and data is reliable. It should not be treated as a magic number. Suppliers must show the sample size, control charts, measurement method, and calculation period. A high Cpk from poorly calibrated equipment proves little. Check the gauges, too.
Real verification often exposes uncomfortable gaps. Some prototype processes are not yet stable enough for capability studies. That is not automatically a failure, but it requires a clear improvement plan. Global buyers can request pilot-run data, nonconformance records, and corrective-action evidence before scaling production. Honest limitations are more valuable than polished claims. Quality still needs questioning.
Global buyers should test a prototyping partner before signing a large purchase order. DFM review is a practical starting point. Engineers should check wall thickness, draft angles, tolerances, material shrinkage, and machining access. A small CAD change can prevent expensive tooling rework. ISO research shows that certified quality systems exceed 1.5 million locations worldwide, but certification alone does not prove process capability.
IP protection needs written controls, not friendly promises. Use project-specific access, encrypted file transfer, employee confidentiality agreements, and clear ownership clauses. WIPO recorded 272,600 international patent applications in 2023. That volume reflects intense global innovation and greater disclosure risk. Ask how files are stored, deleted, and shared with subcontractors. Details matter.
Incoterms define delivery responsibilities, costs, and risk transfer. They do not automatically define ownership, payment security, or product acceptance. State the exact version, named place, insurance duty, and customs responsibility. For automotive or regulated programs, PPAP should include dimensional results, material records, process flow, control plans, and capability evidence. Request a realistic submission level. Level 3 is not always necessary, and assuming it is can waste time. One weakness remains common: buyers approve samples without checking how production conditions will change them. A witnessed pilot run is often more revealing.
The chart compares the number of defined buyer checkpoints used in a practical global sourcing review. DFM covers manufacturability, tolerances, materials, tooling, and production feasibility. IP protection covers ownership, confidentiality, data access, and usage rights. Incoterms review covers the selected rule, named place, cost allocation, risk transfer, and insurance responsibilities. PPAP is represented by its 18 standard submission elements used for production-part approval.